See how CT scanning improves first article inspection for medical devices. Verify internal features, wall thickness, and GD&T before production begins.
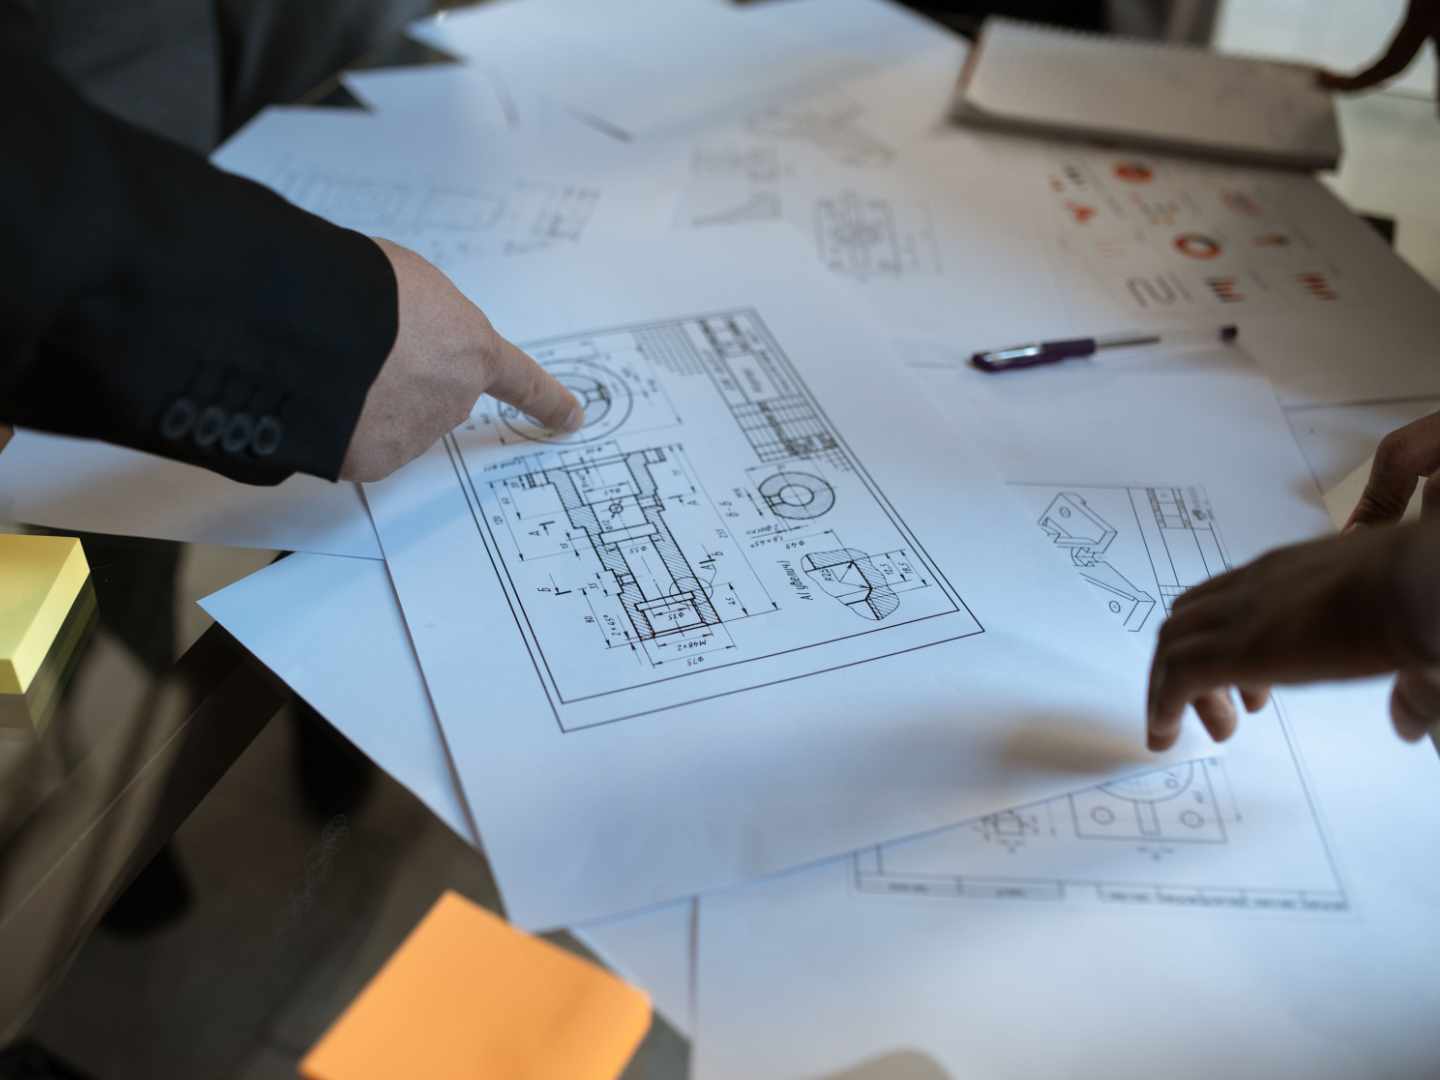
A molded medical part can look right and still be wrong where it matters most. An internal channel may be too narrow. A wall may be thinner than expected. A connector may not line up correctly with the part it needs to mate with.
Finding those problems after tooling is finalized or production has started can mean another mold change, another sample run, and more time spent figuring out what went wrong.
That is where first article inspection for medical devices becomes valuable. Engineering and quality teams get real data from an early production part, which lets them see how the actual piece stacks up against the drawing, CAD model, and all the tolerance requirements before hitting full production.
That’s why manufacturers turn to professional first article inspection services. They want to catch any issues and make sure everything meets strict quality standards right from the start.
What is first article inspection? It is simply a formal process to ensure that the parts you have manufactured are in compliance with all of the design and quality requirements.
The first article inspection process starts with the requirements for the part. That can include dimensions, datums, GD&T callouts, internal features, wall thickness, mating surfaces, and other characteristics that affect fit or function.
The first manufactured parts are then measured against those requirements. Any differences can be reviewed before the same issue is repeated across a larger production run.
For medical-device manufacturers, this type of inspection also fits into a broader quality system. FDA’s Quality Management System Regulation, effective February 2, 2026, requires finished-device manufacturers to maintain systems that help ensure products consistently meet applicable requirements and specifications. FAI can provide useful manufacturing evidence within that larger process, although it does not replace required design verification or validation activities.
The right inspection method depends on what needs to be measured.
A molded part may need external dimensions checked, but it may also contain internal passages, threads, snap features, sealing areas, thin walls, or enclosed geometry. Some of those features are difficult to reach with traditional measuring equipment.
A practical prototype inspection may use more than one method. CMM can handle tight-tolerance measurements on accessible surfaces. Industrial CT can capture internal and external geometry without cutting the part apart. The scan data can also be compared with CAD to show where the molded part differs from the intended design.
For complex medical parts, that combination can give engineers a much clearer picture of what the tooling and molding process actually produced.
CMM is still an excellent choice when a probe can reach the feature and high-accuracy contact measurement is needed.
CT has an advantage when the feature is hidden, enclosed, delicate, or difficult to reach. NIST notes that X-ray CT is well suited to nondestructive dimensional measurement of internal features and can measure geometry that tactile or optical coordinate systems cannot access.
That makes industrial CT scanning services especially useful for parts with internal channels, enclosed cavities, changing wall thickness, internal threads, or assembled components that would otherwise need to be cut or taken apart.
The best choice is not always CT or CMM. Good dimensional inspection services match the measurement method to the part, tolerance, material, and feature being inspected.
Prototype development gets expensive when the team knows a part failed but does not know exactly why.
CT can provide more information from the same physical sample. Engineers can compare the full part to CAD, look at internal geometry, check wall thickness, review hidden interfaces, and see where shape changes occurred during molding.
That can turn a general problem such as “the parts do not fit” into a specific finding about where and how the manufactured geometry changed.
The next tooling or design adjustment can then be based on measured evidence rather than trial and error. CT does not eliminate the need for prototypes, but it can help each prototype answer more questions before another version is made.
A measurement alone doesn’t always tell an engineer if the part will work.
GD&T defines how features relate to one another. It uses controls such as position, profile, flatness, perpendicularity, and runout. Applying GD&T during FAI helps teams judge the manufactured part against its actual functional requirements instead of looking only at basic length or diameter measurements.
This is especially useful when CT or CMM data needs to support a clear pass, fail, or engineering-review decision.
Sometimes there is a physical part but no reliable CAD model. In other cases, engineers want to capture a successful prototype and use its geometry as a starting point for the next design.
Reverse engineering can turn scan or measurement data into usable 3D geometry. CT, CMM, and 3D scanning can support outputs ranging from polygonal scan data to surface models and editable CAD models, making the process useful for product redesign, rapid prototyping, and new tooling.
A good FAI / prototype inspection should answer more than whether a few dimensions passed or failed. It should help your team understand what was actually manufactured, where it differs from design intent, and what should happen before the next production step.
If your medical device has complex molded geometry, hidden features, tight GD&T requirements, or a prototype problem that conventional inspection has not fully explained, send your part, CAD model, and drawing to Nel PreTech. Let our engineering team build the right CT scanning and dimensional inspection plan before the next tooling decision is made.
Jason Johnson is a senior technical leader at Nel PreTech Corporation with degrees in Electrical Engineering (UIC) and Computer Science (Governor’s State University). He oversees CMM, Vision, CT, and Blue Light scanning operations and serves as Quality Manager, maintaining ISO 17025 accreditation. With more than two decades at Nel PreTech, Jason brings deep expertise across metrology, quality systems, and technical operations.

You'll find all the detailed service information you need in one brochure.
Download Brochure
Get a quote within 24-hours and keep your project on schedule.
Get a Quote
Our Nel PreTech engineers are ready to get started on your product challenges.
Ask an Engineer
Download the ultimate CT Scanning Buyer's Guide to improve understanding, time, and efficiency in your scanning needs. Over 50 Pages of useful data and case studies.
Download Now